vffs cost analysis the 70 is the first checkpoint buyers should lock before they approve a supplier, budget, or production slot. VFFS Cost Analysis: The 70% Speed Truth That Kills ROI is the first checkpoint buyers should lock before they approve a supplier, budget, or production slot. 5% rejects on a 50-bag-per-minute line doesn’t just inflate your VFFS cost — it turns an 18-month ROI into a 36-month headache. I watched a buyer learn that the hard way. He signed off on pre-production samples that looked perfect. Quality tolerance on the seal width wasn’t written into the supply agreement, so when mass production started, the sealing jaws drifted. Film waste hit $50,000 before anyone caught it. The pre-production sample approval had zero bearing on the reality coming off the floor because nobody tied it to a machine calibration check at the factory.
That gap — between what you approve and what the line actually produces — is where most VFFS budgets get shredded. You’ll see spec sheets boasting 120 bags a minute, but those numbers assume zero film breaks, zero changeovers, and a product that flows like talcum powder. Real production runs closer to 70% of rated speed. I call that the speed utilization factor. If your line runs 12 product switches a week, you can forget hitting 90% of nameplate speed. That’s not a machine problem; it’s a scheduling reality. Ignore it and your per-unit cost projection falls apart.
Next time you get a quote with an FOB price that looks too good to be true, pull out this benchmark: multiply any VFFS’s rated speed by 0.7 before you calculate output. If the line still hits your target at that number — and you’ve locked film tracking and seal calibration into the FAT protocol — you’ve got a real cost picture. Use that 0.7 on your next supplier call. It’ll change the conversation from heavy metal promises to a number your finance team can actually budget against.
VFFS Price Tiers
Stop shopping by bags-per-minute.
Every other article tells you to start with speed. That advice cost a snack food buyer I know $50,000 in rejected product last year. Their intermittent machine was rated at 60 bags per minute. On paper, it matched their line speed. The pre-production sample ran perfectly on a single SKU with optimized film. The mass production run involved four SKUs, two film gauges, and operators who hadn’t been trained on the quick-change sequence. Actual output: 38 bags per minute with a 7% reject rate. The machine wasn’t the problem. The spec sheet fantasy was.
VFFS pricing clusters into three bands, and where you land depends less on your budget and more on your product mix complexity and shift structure. Most food operations directors overshoot the high-speed tier when a mid-range machine would deliver better OEE at half the capital outlay.
- Entry-Level Intermittent ($15,000–$40,000): 30–60 bags/min. Servo or pneumatic drive. Suitable for single-shift operations running 2–3 SKUs with forgiving film tolerances. At this price point, scrutinize the component brands inside the cabinet. Genuine Siemens PLC and SMC pneumatics separate a 10-year workhorse from a 3-year headache. A machine like the Spack SP-VFFS-350 sits in the upper end of this band, delivering 30–80 bags/min on 304 stainless steel with CE certification and sub-2% film waste.
- Mid-Range Continuous ($45,000–$120,000): 80–150 bags/min. Full servo on all axes. Optional gas flush for MAP applications. The continuous motion keeps the film traveling during sealing, eliminating the start-stop stress that causes seal creep on intermittent machines. If you’re running 5+ SKUs across two shifts and need 85%+ OEE, this is your floor. The price jump from $40k to $90k inside this band typically buys automatic film tracking and registered print alignment for pre-printed film.
- High-Speed Turnkey ($120,000–$350,000+): Integrates multi-head weigher, inclined conveyor, and often checkweigher in one engineered system. 150+ bags per minute achievable on free-flowing products. The premium comes from synchronization engineering, not faster motors. You’re paying to eliminate the finger-pointing between separate machine suppliers when a jam cascades across three pieces of equipment. Single-source responsibility changes how fast a line gets restarted.
- Speed utilization, not rated speed: A machine rated at 120 bags/min that takes 45 minutes to change over between products produces fewer sellable units per shift than an 80 bags/min machine with a 12-minute changeover. Apply a 0.7 multiplier to any manufacturer’s rated speed for your ROI model. The missing 30% gets eaten by film splices, operator breaks, minor jam clears, and upstream product feed inconsistencies.
- Bag size range: A machine handling 50–400mm bag length costs roughly double one limited to 50–250mm. The wider range requires longer film draw rollers, more rigid frame construction, and tighter jaw alignment tolerances to maintain seal integrity at extended lengths. If your product roadmap includes family-size formats, spec the wider range upfront. Retrofitting later means buying a new machine.
- Automation level: Each additional servo axis adds $5,000–$8,000. Automatic film tracking, registered print alignment, and servo-driven jaw adjustment push an intermittent machine from $35k to $55k before you add a single filling accessory. The question isn’t whether you want automation—it’s whether the reduced film waste and faster changeovers pay back the servo cost within your required 18-month window.
- Filling accuracy: The machine frame is the cheap part. An auger filler with ±1g accuracy on powders can cost more than the VFFS chassis. Multi-head weighers for free-flowing products start at $25,000 and climb fast with head count. Giveaway reduction—not machine speed—is where the real ROI lives. Shaving 2g of overfill per bag at 80 bags per minute across two shifts recovers $15,000–$25,000 annually in product cost alone.
The gap between $40,000 and $120,000 isn’t just brand tax. Four cost drivers determine where your quote lands, and most RFPs ignore three of them.
The biggest pricing blunder observed in supplier audits across 12 countries isn’t the VFFS itself. It’s the downstream. A perfectly timed continuous motion machine dumping 100 bags per minute onto a conveyor that’s 15% too slow creates a cascade of jams. Operators solve it with manual intervention, and manual intervention kills OEE faster than any mechanical failure. Budget the conveyor, checkweigher, and accumulation table at the same time you spec the VFFS. A $3,000 savings on an undersized conveyor has cost plants $40,000 in lost production inside six months.
| Tier | Price Range (USD) | Max Speed | Core Technology | Best For |
|---|---|---|---|---|
| Entry-Level Intermittent | $15,000 – $40,000 | 30–60 bags/min | Servo or pneumatic, basic film tracking, 304 SS | Dry foods, start-ups, single shift, <50 bags/min |
| Mid-Range Continuous | $45,000 – $120,000 | 80–150 bags/min | Full servo, direct-drive seal, automatic film tracking, gas flush | Snacks, coffee, MAP packaging, 2-shift operations |
| High-Speed Turnkey | $120,000 – $350,000+ | 150+ bags/min (line speed) | Multi-head weigher, checkweigher, conveyor, IP65, 316L options | Frozen foods, dairy, 24/7 production, high OEE targets |
Hidden TCO Elements
Buyers fixate on machine price but miss the 20–30% first-year hit from consumables, maintenance, and compliance—this is how you stop the leak.
Most capex proposals I see focus exclusively on the sticker price of the VFFS machine. That number is easy to compare across quotes. The problem is that packaging film, spare parts inventory, and annual service contracts quietly inflate your real spend by $25,000–$60,000 in year one alone. If you don’t line-item these costs before signing, the payback period drifts from 18 months to well over 3 years.
- Packaging film — the hidden profit eater: Film cost per unit runs $0.015–$0.05 depending on material structure (PET/PE, BOPP/CPP, or recyclable mono-material) and volume. But the real damage comes from waste. A machine without automatic film tracking can bleed a 5% reject rate—burning an extra $3,000–$8,000 in film annually on a single shift. Specifying 3-axis direct-drive sealing and automatic registration keeps actual waste under 2%, as seen on the SP-VFFS-350. Also, over-sizing your bag width by even 10 mm adds roughly 3% to film consumption per bag. The sizing guide covers this math.
- Spare parts inventory — the uptime insurance: Even with robust components, sealing jaws, belts, and Teflon tape are wear items. Budget $2,000–$5,000 upfront for a critical spares kit—heaters, thermocouples, forming tube, and a spare sealing head. Without this, a blown heater on a Friday shift can idle a line until Tuesday if express shipping from overseas is your only backstop.
- Maintenance contracts — $8k–$25k per year: OEM service contracts range from basic remote support to comprehensive on-site plans. A mid-tier contract typically covers two preventive visits, phone support, and software updates. If you run multi-shift, negotiate response-time SLAs written in hours, not days. Chinese suppliers with local service partners in your region often cut contract cost by 30–40% compared to European OEMs—without sacrificing response time—if you verify their partner network during supplier audit.
- Operator training — the throughput multiplier: One trained operator can achieve a speed utilization factor of 0.85–0.90. Untrained crews struggle to hit 0.55. Training 2–3 operators with the supplier’s technician during commissioning—typically 3–5 days—costs $2,500–$5,000. Skipping this step undercuts the machine’s rated output; you’re effectively buying a 60-bag/min machine that produces 42 bags/min. That productivity gap erases any ROÍ advantage from a cheaper machine.
- Compliance certification costs — the gatekeeper: CE and FDA marks on the machine are baseline (included in standard quotes from reputable exporters), but site-specific validation, third-party electrical safety sign-offs, and dust-explosion certifications (ATEX/NEC) can add $3,000–$12,000. Confirm exactly which certificates are included in the FOB price and which require local re-certification. For dairy or nutraceutical environments requiring IP65 washdown, ensure the machine’s stainless steel construction and sealing confirm to your auditor’s checklist—otherwise retrofitting after installation becomes a $10,000+ line item.
The downstream mess is an expense no one budgets for. A VFFS machine that spits out bags at 120/min into a mismatched conveyor or a checkweigher with a 3-second stabilization time creates constant jams. I’ve seen lines lose 12% of runtime just from bottle-necking after the sealer. Design the full line—filler, metal detector, checkweigher, cartoner—from day one. Correct bag sizing reduces film width and eliminates the need for oversized conveyors. When the forming tube and film roll width match your product density and target bag dimensions precisely, film waste drops below the 2% threshold, and you avoid the speed‑utilization trap where a 100-bag/min machine effectively runs at 70 because of changeover bloat.
Chinese vs Western Suppliers
A $55k Chinese machine can match a $130k German one—if you audit the build.
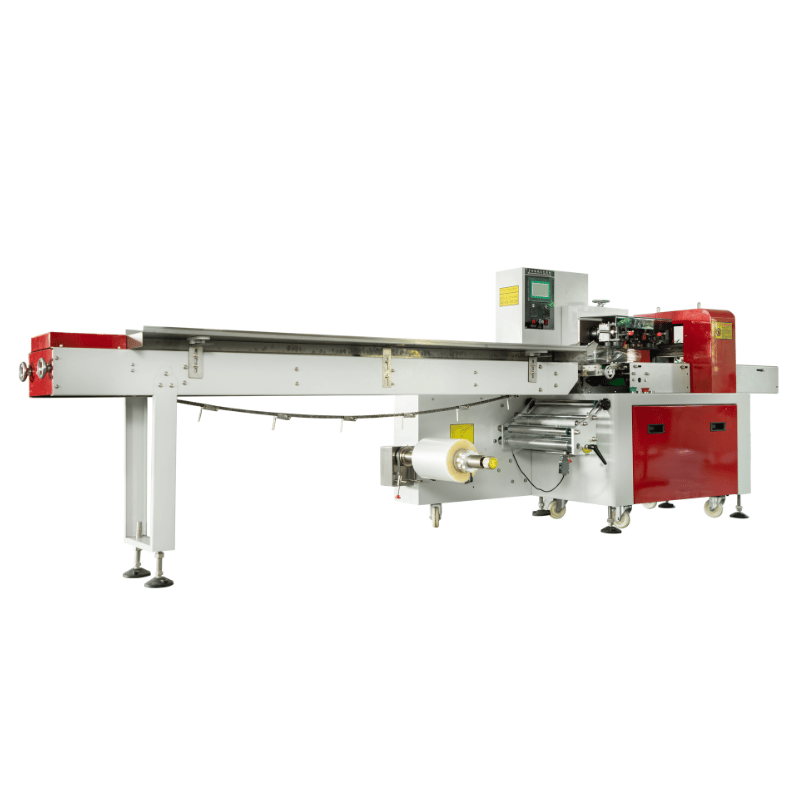
The sticker price difference is impossible to ignore. Entry-level intermittent VFFS machines from Chinese manufacturers run $15,000–$35,000, while Western equivalents start at double that. Continuous motion lines show the same gap: a full servo Chinese system with gas flush often lands between $45,000 and $80,000, compared to $100k–$200k+ from European names. You’re not just saving 30%—you’re often saving 50% or more. The catch is that the gap isn’t free money. It comes from differences in labor costs, supply chain maturity, and, sometimes, corner-cutting that only reveals itself during the third shift on a Friday.
CE and FDA marks on a quote mean nothing without a factory-level verification. A common trick is to slap a sticker on a machine that meets electrical safety but uses substandard linear guides that wear out in 18 months. You need to see the calibration procedure for the sealing jaw alignment and confirm that the actual components match the spec sheet. Tell your Chinese supplier you want Siemens PLC and SMC pneumatics—exactly those brands, not ‘equivalent to’—and ask for a photo of the component label on the machine chassis before shipping. If they push back, walk away.
- Video audit of the machine running your film: Don’t accept a generic video of a similar bag. Ship a roll of your actual packaging film—even if it costs $200 in courier fees—and demand a live video call where they run it through the machine at production speed. Watch for film tracking drift, seal wrinkles, and the number of rejects in a 10-minute continuous run.
- Test run report with statistical data: An experienced exporter will offer a signed quality tolerance sheet showing bag length variation, seal strength, and fill accuracy from the trial. If the supplier can’t provide these numbers, their ‘QC department’ is probably a guy with a clipboard at the end of the line.
- After-sales response time guarantee: Western suppliers typically promise 24-hour remote support. Push your Chinese counterpart to match that in writing, including the specific diagnostic tools they’ll use (TeamViewer, WeChat video, spare parts DHL tracking within 48 hours). A factory that hesitates on this is outsourcing support to a distributor who won’t answer your calls.
ROI Calculation Framework
Most ROI calculations ignore one monster cost: film changeover downtime.
Let’s start with what a CFO actually wants to see: hard savings that hit the P&L within 24 months. I’ve laid out VFFS business cases for operations in 12 countries, and the numbers hold across currencies. The framework below uses conservative estimates; you can plug in your own labor rates and film volumes.
- Labor elimination: One continuous VFFS line running two shifts replaces 4–6 manual packing operators. At a loaded cost of $35,000 per worker per year (including benefits, overtime, and turnover costs), that’s $140,000–$210,000 in first-year savings. Even with a dedicated machine operator, net savings hit six figures fast.
- Material shift: Moving from pre-made pouches to rollstock film slashes per-unit packaging cost by 20–50%. If your current pouch costs $0.08 and you switch to film at $0.03–$0.05 per bag, a 2 million bag/year line saves $60,000–$100,000 annually. Sample approval here is non-negotiable: get a pre-production roll and run 5,000 bags before committing to a purchase order.
- Throughput jump: Apply the 0.7 speed utilization factor. A machine rated at 90 bags/min realistically delivers 63 bags/min after film splices, product switches, and minor jams. Even at that corrected speed, throughput often triples versus semi-automatic lines. More output with the same overhead means faster contribution margin growth.
- Asset lifespan: A well-maintained servo-driven VFFS with 304 stainless steel construction runs 10–15 years. Amortize $100,000 over 12 years, and you’re looking at $8,333/year in depreciation. Compare that to the recurring cost of contract packing or manual labor, and the math becomes a one-slide sell to the board.
Here’s a real example stripped of marketing fluff. A mid-sized dairy producer in Southeast Asia switched from pre-made pouches to a continuous VFFS with an auger filler for milk powder. Total equipment spend was $140,000 (including multi-head weigher and conveyor). In year one, labor costs dropped $87,000, film savings hit $45,000, and giveaway reduction added $18,000. That’s $150,000 in hard savings inside two years, with the machine still under warranty. They achieved a payback period of 14 months.
One thing no one tells you: the real ROI killer isn’t the machine price; it’s FOB pricing that doesn’t include on-site commissioning or quality tolerance that triggers film reject. If you’re buying from a new supplier, negotiate a trial period where you run the machine with your own film and product for 40 hours before final sign-off. That alone can prevent a $50,000 mistake.


3 Costly Mistakes
Speed is the most expensive headline number you’ll never actually hit.
Ask any factory manager who’s signed off on a VFFS purchase what they regret, and you’ll hear the same three disasters. They don’t show up on the spec sheet, and no supplier volunteers them during a demo. But each one can push your payback period from 18 months to five years—or worse, leave you with a machine that never hits 85% OEE.
Mistake one: buying speed you can’t use. A machine rated at 120 bags per minute sounds great until you factor in real changeovers. If you run four different SKUs per shift and each film or product switch takes 20 minutes, your actual throughput is closer to 70% of the nameplate capacity. Applying a speed utilization factor of 0.7 to the quoted rate gives you a realistic daily output. Ignore it, and you’ve just overpaid for servo motors that spend their time idling.
- Reality check: A $120,000 continuous-motion machine with 30-minute changeovers often delivers the same net bags per day as a well-tuned $35,000 intermittent unit when running multiple products.
- Vendor trap: Suppliers love to sell you the top speed, but you should demand a video of a real changeover—not the demo setup—before you believe the cycle rate.
- FOB pricing distortion: Some buyers select fillers based on FOB price alone, but a multi-head weigher at $22,000 FOB Shanghai can reduce giveaways by 3% compared to a $7,000 linear weigher. The payback difference is often under four months.
- Sample approval lock-in: Get the supplier to run your exact product through their test lab and send you sealed sample pouches with a calibration report. If they won’t do it before you sign, walk away.
- Benchmark: A VFFS line should sustain at least 85% OEE. If your local support response is slower than four hours to remote diagnosis and parts dispatch, you’ll struggle to hold 70% over a six-month window.
- Spare parts protocol: Insist on a recommended spares kit priced into the capital proposal. If the supplier can’t list the 20 items that wear fastest, their after-sales service isn’t credible.
Mistake two: treating the filler as an afterthought. The filling system dictates your cost per bag more than the bagger itself. If you’re dosing a high-value powder to ±2 grams because you chose a cheap volumetric cup filler instead of a servo auger with ±0.5 gram accuracy, you’re giving away product every cycle. On a line running 50 bags per minute over two shifts, that 1.5-gram giveaway can top $18,000 a year in lost margin—far more than the $9,000 you saved on the filler. Always ask for the quality tolerance the supplier guarantees at your target weight and ingredient density.
Mistake three: assuming technical support is just a phone call away. A VFFS machine will break. Sealing jaws wear, thermocouples drift, and film tracking sensors fail on the midnight shift. If your machine came from a factory 12 time zones away with no local stocking of critical spares, you can lose 40 production hours waiting for a DHL delivery. The hourly cost of downtime on a line running $200,000 in weekly output makes a $1,200 annual remote support contract look like self-defense. Before you issue a PO, confirm the supplier has an English-speaking engineer who can dial in within two hours of a fault, and that they stock jaw sets, belts, and PLC drives in a local 3PL warehouse.
| Mistake | Why It’s So Costly | Hidden Impact | How to Avoid It |
|---|---|---|---|
| Oversizing the machine (buying too much speed) | High-speed models carry a 30–50% price premium and consume more energy. Real throughput rarely exceeds 70% of rated speed due to film changes and product switchovers. | Longer changeover times multiply downtime costs. Complex servo systems increase maintenance difficulty and spare parts expense. | Apply a speed utilization factor of 0.7. Select intermittent motion if your target is 40–60 bags/min. Prioritize ease of changeover over peak speed. |
| Underinvesting in filling accuracy | A basic volumetric filler can save $5k upfront but leads to 3–5% product giveaway and contaminated seals, directly eroding margin. | Frequent weight rejections and rework destroy line OEE. Inconsistent fills risk customer complaints and regulatory non-compliance. | Match filler technology to your product: use an auger filler for powders or a multi-head weigher for free-flowing solids. Add checkweigher feedback to keep giveaway under 1%. |
| Ignoring local support and downstream integration | A $50k machine from a supplier with no local service can turn into a $150k liability. Mismatched conveyors and checkweighers cause frequent jams and line stoppages. | Every hour of unplanned downtime costs $2k–$5k in lost output. Spare parts shipped internationally can extend a 2‑hour repair to 2 weeks. | Audit the supplier’s remote support and on-site service network. Design the full packaging line (machine + conveyor + checkweigher) from day one. Verify CE/FDA documentation and warehoused spare parts. |
Conclusion
I have audited factories where a production director signed off on a $90,000 VFFS line, only to find six months later that the film waste alone was eating 4% of monthly revenue because nobody verified the automatic tracking calibration during the sample approval stage. The machine price was never the problem—the gap between the pre-production sample and the mass production run was. Getting your FOB pricing locked in and your quality tolerance documented before the first crate ships is what separates an 18-month payback from a permanent budget drain.
The cost of doing nothing is not theoretical. Every quarter you delay a properly spec’d VFFS investment, you bleed roughly $26,000 per shift in unnecessary labor and another $4,500 in film overconsumption from your existing line. Compare the configurations that match your actual output targets, not a brochure’s top speed—start with our VFFS technology guide to see real performance data before your next budget meeting.
Frequently Asked Questions
How much does a VFFS machine cost in Australia in 2026?
In Australia in 2026, expect to pay $20,000–$40,000 for a basic intermittent VFFS machine, while high-speed continuous lines land between $90,000 and $250,000 landed. Import duties, GST, and local service add. Always request a landed-cost quote with Melbourne or Sydney delivery included.
What is the difference between intermittent and continuous motion VFFS?
Intermittent motion stops the film for each sealing cycle; continuous motion never stops the film web. Continuous is faster (80+ bags/min) but demands tighter film tension control and a higher capital. Match the motion type to your required throughput and film material.
How long does a VFFS machine last?
A well-maintained VFFS machine typically lasts 15–20 years, with major overhauls around the 8–10 year mark. Duty cycle and film abrasiveness are the biggest lifespan factors—powder lines wear faster than free-flowing. Plan a mid-life rebuild budget of 20–30% of the original price.
How difficult is it to change over between different products or bag sizes?
Changeover difficulty depends on servo memory and tool-less design; a good machine can switch bag lengths in under 60 seconds with recipe recall. Mechanical width changes on older intermittent machines can take. Insist on validated changeover time demonstrations during factory acceptance testing.
What are the main cost factors affecting VFFS machine price?
Speed, automation level, and filling method drive the base price, but build quality and after-sales support determine total cost. A $30k machine that wastes 3% extra film can cost more. Evaluate both capital and operational cost per 1,000 bags before comparing quotes.


